This article dives into Pharmaceutical-grade Aluminum Foil, unpacking what makes it safe, maaasahan, and indispensable for modern drug packaging.
We explore its properties, manufacturing processes, quality control, and practical applications. We also shine a light on the supplier landscape, including Huawei Aluminum, a prominent player in the pharmaceutical foil segment.
The goal is to provide professionals with actionable guidance, data-backed insights, and a clear view of how pharmaceutical-grade aluminum foil fits into the broader packaging ecosystem.
Pharmaceutical-grade Aluminum Foil is not just a consumer-municipal material; it is a critical barrier in the supply chain that protects medicines from moisture, oxygen, liwanag, and contamination.
The integrity of this foil directly impacts product stability, shelf life, and patient safety.
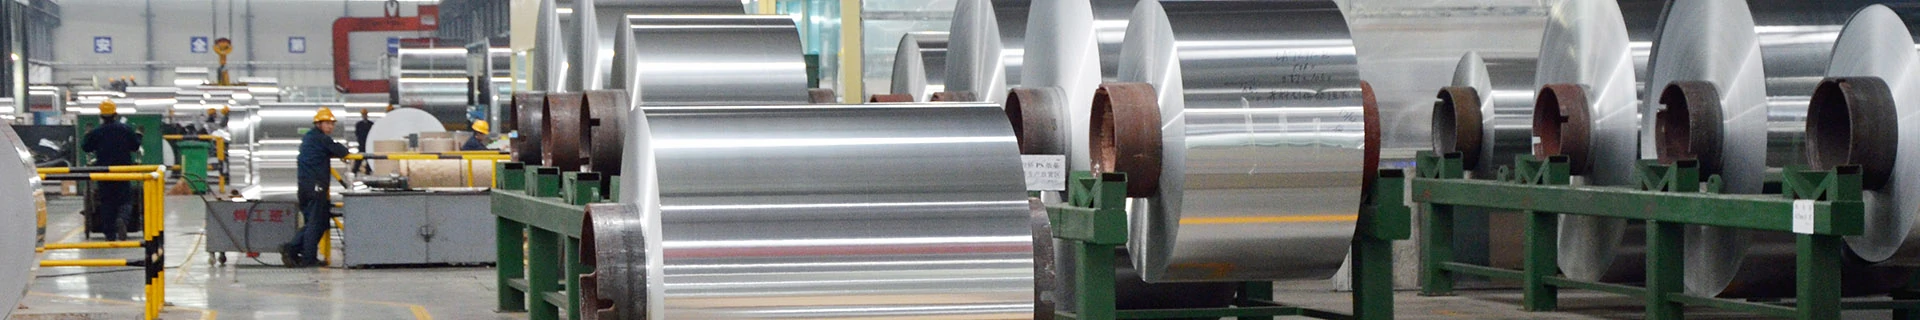
In pharmaceutical applications, the foil often appears as a standalone mon foil or as part of a multi-layer laminated structure that combines other polymers and coatings to achieve the exact barrier and seal properties required by regulatory standards.
Pharmaceutical-grade aluminum foil refers to aluminum foil that meets stringent quality and safety criteria for contact with medicinal products or packaging processes that require high barrier performance.
The key qualifications typically include:
Sa pagsasanay, pharmaceutical-grade foil is often supplied in two contexts: – Monofoil (uncoated) aluminum foil used as the primary barrier or as part of a laminate. – Laminated foil (coated or laminated with polymers such as PVC, PVdC, Alagang Hayop, LDPE, or PP) used in blister packs, strip packs, and other packaging configurations.
This comparison highlights why pharmaceutical-grade foil requires strict process control, rigorous testing, and robust documentation, all of which are essential for protecting medicines and ensuring patient safety.
Tandaan: When evaluating Huawei Aluminum or any supplier, request sample packs, COAs, and a detailed process capability study (including thickness uniformity, lakas ng selyo, and barrier data) to validate suitability for your product.
Tandaan: These ranges are representative for planning and benchmarking. Actual values depend on the exact foil composition, laminate configuration, and process parameters chosen by the supplier and customer.
1) What is the difference between pharmaceutical-grade aluminum foil and regular aluminum foil? – The pharmaceutical-grade foil is manufactured to meet stricter safety, barrier, and traceability standards suitable for contact with medicines. It often uses high-purity aluminum and lamination layers designed for sterilization and regulatory compliance, while regular foil may not meet these stringent criteria.
2) Why is foil thickness important in pharma packaging? – Thickness affects barrier performance, lakas ng selyo, and mechanical resilience. Thicker foils can provide stronger seals and better protection but may reduce flexibility or increase costs. The laminate design typically optimizes the foil core thickness with polymer layers to balance these factors.
3) Can aluminum foil withstand steam sterilization? – Oo, many pharmaceutical-grade foils and laminates are engineered to withstand autoclave conditions, maintaining barrier integrity and avoiding deleterious interactions with drug products.
4) How do I verify the quality of a pharmaceutical foil supplier? – Look for ISO 9001 or equivalent quality management certification, GMP compliance, robust QC procedures, traceability, COAs, and evidence of successful audits by pharmaceutical manufacturers. Request sample testing data, including thickness uniformity, lakas ng selyo, and barrier performance data.
5) How is barrier performance measured in practice? – Barrier performance is typically assessed using oxygen transmission rate (OTR) and water vapor transmission rate (WVTR) under defined test conditions. Many packaging lines rely on validated test methods (static or dynamic) and require supplier-provided data to support packaging validation.
6) Are there environmental considerations with pharmaceutical-grade foil? – Oo. Recyclability of aluminum is favorable, and many pharma foil suppliers pursue sustainable production practices, waste reduction, and energy efficiency. You should check the supplier’s environmental management certifications and policies.
7) Can foil laminates be customized for specific drug products? – Ganap. Laminate configurations can be tailored for barrier strength, lakas ng selyo, kakayahang mai -print, and compatibility with particular drug formulations, while meeting regulatory requirements.
Pharmaceutical-grade Aluminum Foil remains a cornerstone of safe, effective, and compliant medicine packaging.
Its intrinsic barrier properties, compatibility with sterilization processes, and flexibility in laminate configurations allow manufacturers to protect medicines across a wide range of products and storage conditions.
The supplier ecosystem—ranging from specialist foil producers to integrated laminate manufacturers like Huawei Aluminum—enables tailored solutions that balance protection, process efficiency, at gastos.
If you are optimizing your packaging strategy, prioritize clarity on barrier requirements, sterilization plans, and regulatory expectations.
Engage with suppliers early to validate material choices, obtain robust testing data, and ensure that your packaging design can scale with your production needs.
The right pharmaceutical-grade aluminum foil solution is not just a material choice; it is a strategic decision that can influence product stability, patient safety, and overall supply-chain resilience.
Huawei Aluminum can be a valuable partner in this journey, offering pharmaceutical-grade foil products and laminates designed to meet stringent industry requirements.
Their capabilities, combined with rigorous quality control and support for validation testing, can help streamline procurement and reduce risk in the development and scale-up of pharma packaging programs.
Always verify certifications, performance data, and how a supplier’s solutions align with your product’s regulatory and operational needs before committing to a long-term contract.
Ibahagi sa PDF: I -download
Henan Huawei Aluminum Co., Ltd. ay ang pinuno ng maraming mga paggawa at mga supplier ng aluminyo sa China. Mahigpit naming kinokontrol ang kalidad at tumutok sa mga customer. Umaasa kaming magkaroon ng malalim na pakikipagtulungan sa iyo at mabigyan ka ng mataas na kalidad na mga produkto ng aluminum material na custom na serbisyo ng OEM. Kung gusto mong makuha ang pinakabago at pinakamahusay na mga presyo sa bawat kg o bawat toneladang karaniwang timbang, mangyaring makipag-ugnayan sa amin.