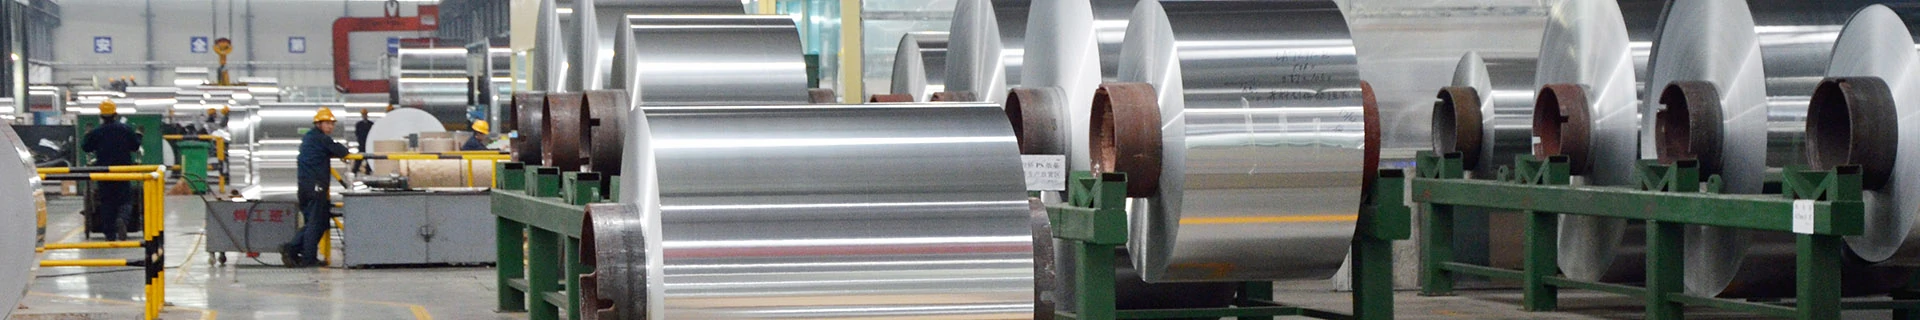
An 8011 aluminum foil jumbo roll is the wide, large-diameter mother roll that flexible packaging converters, household-foil winders, food-container plants and pharmaceutical packaging producers buy before they slit, laminate, print, coat or press it.
It is the semi-finished, converter-grade form of the same 8011 foil that ends up as a kitchen roll, a printed pouch, a heat-seal lid, a takeaway tray or a medicine blister.
Buying the correct jumbo roll controls the barrier quality, pinhole count and runnability of every finished product made from it.
8011 is an iron-and-silicon alloy that rolls to very thin gauges with high strength, few pinholes and good pinhole resistance, which is why it is the workhorse alloy for food and pharma packaging foil.
For a converter the decisive factors are not the alloy name alone but gauge consistency, flatness, a clean degreased surface, controlled splice count and reliable lot documentation.
This guide explains what a jumbo roll is, how it is made and specified, which converter applications it serves (with flexible packaging and household conversion in the most detail),
how to audit quality and compliance, and how to order from a Chinese mill such as Henan Huawei Aluminum Co., Ltd.
Aluminum foil is rolled aluminum thinner than about 0.2 mm. A jumbo roll—also called a parent roll, mother roll or master roll—is the full-width coil produced at the foil mill before it is cut into narrower rolls.
It is wound on a paper, steel or aluminum sleeve, typically with a 76 mm or 152 mm inner diameter, and is much wider and heavier than a retail product: widths commonly run from 100 sa 1600 mm and a single roll can weigh hundreds of kilograms to over a tonne.
8011 is an 8xxx-series alloy with iron and silicon as the main additions.
Iron refines the grain and raises tensile and puncture strength, while silicon improves hardness and rolling uniformity across a wide web.
The result is foil that is strong at light gauges, low in pinholes and easy to anneal, slit, laminate and print.
Most packaging jumbo rolls are supplied in the soft O temper, which is degreased and fully recrystallized for the highest formability and a clean printing surface.
The distinction from a finished product matters for buyers: a jumbo roll is sold by the tonne to converters who add the conversion—slitting, laminating, paglilimbag, patong, embossing or pressing—whereas a finished household roll or container is sold by the piece.
The jumbo roll is therefore priced and specified like an industrial raw material, with gauge, lapad, core, outer diameter, weight and surface quality agreed up front.
Converters compare offers using a shared jumbo-roll vocabulary.
The sleeve is the inner core; the eye is the circular opening when the roll stands on its flange; eye-to-sky means the core axis is horizontal and the eye faces upward, while eye-to-wall means the roll lies on its circumference.
The outer diameter, roll width and net weight define how the coil fits the unwinder and crane; the splice count states how many joined sections are allowed in a roll.
All of these are fixed by the converter’s equipment rather than by the alloy.
This article covers converter-grade 8011-O aluminum foil; a related technical note on the packaging alloys compares 1235 aluminum foil for composite flexible packaging at 3003 aluminyo palara.
Jumbo rolls are made in several packaging alloys, and the grade should follow the gauge, forming process and end use. 8011 is the balanced default for most food and household foil; the others are chosen for ultra-thin laminating, special strength or heavy containers.
Sa pagsasanay, 8011 is specified for the widest range of food and household conversions because it combines the strength to survive slitting and forming with the pinhole resistance needed at 9–25 µm.
Converters laminating very thin (6–9 µm) barrier webs often use 1235 o 8079, while plants pressing heavy trays may use 3003 o 8021.
The mill should confirm the alloy from the exact gauge and downstream process.
Many converters run more than one alloy in the same plant: a laminate line may use 8011 for medium gauges and 1235 o 8079 for the lightest barrier webs, while a container plant alongside it uses 8011 for standard trays and 3003 for heavy ones.
Buying from one mill that produces the full range simplifies the comparison and avoids switching suppliers when a product changes gauge.
Alloy substitution should be made by the mill and converter together and confirmed by a sample run; halimbawa, a 1235 web cannot always replace 8011 at the same gauge because it is softer and has different strength and pinhole behavior.
Gauge sets the end product: double-zero light foil (roughly 4.5–9 µm) is used in high-barrier laminations, standard household and wrapping foil runs 10–25 µm (heavy duty to 40 µm), and container foil is 40–200 µm.
The soft O temper is the mainstream for household, lidding, pouches and trays because it is fully degreased and easy to convert.
Buyers should specify the gauge tolerance, lapad, core, sleeve material, maximum splice count, outer diameter and roll weight, and the wetting (wettability) grade needed for printing or laminating.
Roll geometry matters for the converter’s equipment: the core must fit the unwinder, the outer diameter and weight must fit the crane and line, and the eye direction (the orientation of the wound web) is matched to the machine.
A jumbo roll that does not match the line’s mechanical limits causes downtime even when the metal itself is perfect.
Most packaging foil starts with twin-roll continuous casting, where molten aluminum solidifies between chilled rolls into a thin strip, followed by repeated cold-rolling passes to the target gauge.
The thinnest gauges are produced by double rolling two foils together, which gives the faces that touch the polished rolls a bright finish and the faces touching each other a matte finish.
Food- and pharma-grade foil is rolled with food-safe oil and produced in clean conditions to keep it free of residue and off-odor.
The coil is then annealed in a controlled-atmosphere furnace to the soft O temper and to deg rease the surface, which is essential for printing, patong, lamination and food contact.
The finished jumbo roll is inspected online for gauge and pinholes and, where the customer needs narrower stock, slit on a precision line.
Iron and silicon in 8011 refine the grain and cast structure so the web rolls to very thin gauges with fewer pinholes than pure aluminum.
Tension control, flatness and edge quality at this stage determine whether the foil runs cleanly on high-speed converters.
Pinholes form at the thinnest gauges where the web approaches the natural rolling limit, and their number is controlled by melt cleanliness and filter fineness, roll polish, rolling-oil quality and the grain refinement that iron and silicon provide in 8011.
Double rolling introduces the matte and bright faces, and the final anneal is timed both to soften the metal to the O temper and to burn off residual rolling oil without oxidizing the surface.
A consistent anneal cycle is what gives a clean, low-odor, print-ready web; under-annealing leaves oil and hardness, while over-annealing can dull the surface and waste energy.
This process control is the main difference between a converter-grade mill and a low-cost trader reselling generic stock.
The largest converter use of 8011 jumbo rolls is the barrier layer of flexible packaging.
The foil is laminated with plastic films (Pe, Pp, Alagang Hayop), paper or adhesives to make retort pouches, coffee and tea bags, snack and confectionery wraps, powdered-food and pet-food bags, doypacks, sachets and composite cartons.
The foil layer is almost always the only component that is truly impermeable to light, oxygen, moisture and aroma, which gives ambient shelf life without refrigeration.
On the converter line the jumbo roll is unwound, printed, often lacquered or coated, and laminated to the other webs before being formed and sealed into packs.
This demands a degreased surface with good wettability and a flat, wrinkle-free web at a consistent gauge, because any pinhole, edge defect or tension variation is multiplied across millions of laminated packs.
For very thin 6–9 µm barrier webs, converters may use 1235 o 8079; for the broad 9–30 µm range, 8011 offers the best balance of barrier and runnability.
A laminated structure is named from the outside in. A common retort structure is PET/adhesive/AL/adhesive/PA/RCPP; a dry-goods coffee pouch may be PET/AL/PE or PET/VMPET/PE; a sealable lid web may be lacquer/AL/heat-seal coating.
The foil layer is the functional barrier, the outer films provide strength and printability, and the inner film provides heat sealing and chemical resistance.
Gauge follows the content: dry foods often use 6–9 µm foil, moist or fatty foods and retort packs use 9–12 µm or more, and liquid or long-shelf-life packs use the higher end.
Because the foil is only a few microns thick in a laminate, any pinhole becomes a diffusion path for oxygen and water vapor, so lamination converters specify the tightest pinhole grades at the lightest gauges.
Surface wettability and degreasing decide whether the adhesive and printing ink wet and bond; a low-wetting or oily web causes pinholes in the print, poor bond strength and delamination.
This is why the same alloy can behave very differently depending on how the mill controlled annealing and surface cleanliness.
Many converter problems trace back to the jumbo roll rather than the line. A short diagnostic table helps buyers specify the right roll and reject out-of-tolerance material before it reaches a long production run.
A second major outlet is the household-foil winding industry, which buys wide 8011 jumbo rolls and slits and rewinds them onto cardboard cores in supermarket widths (commonly 300 mm at 450 mm) and lengths, then packs them into color dispenser boxes.
The same jumbo stock serves catering and heavy-duty brands, embossed and non-stick foil and value or premium retail tiers.
For household conversion the jumbo roll must unwind without wrinkling, telescoping or breaking, slit cleanly into a narrow web, and rewind with even tension so the retail roll is firm and square.
Standard kitchen foil is about 10–15 µm and heavy-duty 18–25 µm or more; 8011 is preferred because its strength and pinhole resistance let a light web tear cleanly by hand and wrap without leaking.
The mill supplies a free end or agreed splice count, a uniform core and stable gauge so the winder’s line runs at high speed with minimal stops.
Household conversion is a high-speed slitting and rewinding operation: the wide jumbo roll is unwound, cut into the retail width by circular or shear blades and rewound onto small cardboard cores, often with a serrated edge, before the rolls are cut to length and boxed.
The economics depend on running the line with minimal stops and scrap, so the mother roll must be round, tightly and evenly wound and free of telescoping, weaving and soft spots.
A loose or off-gauge jumbo roll produces retail rolls that bulge, unwind badly or fail to fit the box, so household winders audit run-out, tension and edge quality roll by roll.
Embossed or non-stick retail foil is usually produced by the mill or a coater before final slitting, and the same 8011 stock supports colored or printed private-label packaging.
Mas makapal 8011 jumbo rolls (roughly 40–200 µm) are pressed into semi-rigid food containers—takeaway trays, round and oval baking pans, airline meal boxes, tart molds, BBQ trays and large catering pans—with ribs and beads stiffening a thin wall.
Intermediate gauges (often 30–45 µm) are coated and slit for heat-seal lids for yogurt, dairy, dessert and ready-meal cups, and printed or lacquered 8011 is used for bottle caps and closures.
These jobs require soft O stock, clean surfaces and container-specific flatness.
In an inquiry the converter should state the application and the lamination or container structure as well as the bare numbers, because the recommended gauge tolerance, surface and wettability differ:
a double-zero laminate needs a tight pinhole grade but a relatively loose forming tolerance, while a container tray needs a consistent temper and a flat web for feeding.
Sharing the end structure, converting speed and target certification lets the mill select the right jumbo roll instead of simply quoting the cheapest gauge.
Container makers and lid converters select the gauge from the tray depth, seal process and food weight; see 8011 foil for food containers for typical container and lid stock, at 3003 aluminyo palara for heavier, more rigid trays.
Beyond food, 8011 and related packaging foils are printed and coated for pharmaceutical packaging—lidding foil for blister packs, push-through PTP foil and, in other alloys, cold-form alu-alu stock—where pinhole-free, clean web and tight documentation are critical.
Other jumbo-roll conversions include cable wrap and shielding (madalas 1235), battery-foil processing, heat-seal and converter foil, labels and hair/beauty foil.
For regulated pharma work the mill supplies the additional certificates and clean production records the packaging standard requires.
Push-through blister packs use a rigid thermoformed PVC or PVC/PVDC base sealed to a printed and lacquered aluminum lidding foil that a patient presses through, while cold-form alu-alu packs use an oriented-polyamide/aluminum/PVC laminate stamped into cavities for moisture-sensitive medicines.
In both cases the foil is the barrier that protects the dose, so pharma converters require pinhole-free web, tight gauge, verified cleanliness and full batch traceability.
The mill supplies the foil in the annealed, degreased condition and documents each coil against the pharmaceutical packaging standard, with pharma-grade packaging and segregation from industrial stock.
A jumbo roll is judged on how it runs on the converter line, not just on chemistry. The critical parameters are:
The mill verifies these with online beta or X-ray gauges, optical or light pinhole tests, tensile and elongation samples, wettability tests and surface inspection, and identifies each jumbo roll by lot so the mill certificate, packing marks and goods all match.
A first-order production sample run on the customer’s own line is the most reliable way to confirm the gauge, surface and winding before a container order.
Pinhole count rises sharply as the foil gets thinner and is specified against the gauge, typically measured with a light table or an online optical detector and reported per square meter.
Surface wettability is checked with test liquids (a common print or lamination target is around 32 mN/m or higher), and degreasing is graded by a water-spread or washing test.
Tensile strength and elongation are pulled from coupons, while flatness is checked on the unrolled web for waves, buckles and crossbow.
Because these measurements are destructive or sampled, the lot number links the certificate, the coil tag and the shipped roll so that a claim or recall can be traced to the cast and anneal cycle.
8011 dominates converter-grade foil because it is the most economical alloy that still delivers the barrier, strength and pinhole resistance packaging needs.
Its iron and silicon add puncture and tensile strength at thin gauges, so a web of 8011 performs like a thicker pure-aluminum web while using less metal; the annealed O surface is clean and easy to print, coat and laminate; and the alloy tolerates high-speed slitting, rewinding and forming.
It is supplied in very wide jumbo widths that converters use efficiently, and the same mill can match the gauge to pouches, household rolls, lids or containers.
Aluminum is also fully recyclable and hygienic, which supports food-brand and sustainability requirements.
The alloy also converts efficiently: at the same strength it can run lighter than pure aluminum, reducing the metal weight in a pouch or lid and lowering the cost per thousand packs;
it is compatible with the standard adhesives, inks and heat-seal coatings already installed in converter plants; and it is stable at the high temperatures used in retort sterilization and hot filling.
Clean foil trimmings and lamination scrap can be recovered, which supports brand and regulatory targets for recyclable packaging and reduces converter waste.
Buyers should request a lot-specific mill certificate and, for food or pharma contact, the food-contact declaration or migration report; coated or laminated foil also needs food-grade coating and ink documents.
Certification should be tied to the actual lot rather than issued as a generic company statement.
A practical document set for a converter shipment includes the mill certificate, the food-contact declaration and migration test (often renewed annually or per product), the alloy and temper record, dimensions and gauge report, and the packing list and certificate of origin.
For pharma, buyers additionally request the pharmaceutical packaging compliance and, for laminated or coated material, the food-grade status of every coating and ink.
It is good practice to keep the same lot number on the coil tag, the invoice and the certificate so that any end-customer audit can be answered without delay.
Jumbo rolls are fragile and heavy, so they are packed to protect the edges and surface from moisture, crushing and mechanical damage.
Each roll is normally wrapped in moisture-proof film or VCI/protective paper with end protectors, supported on a wooden pallet or in a wooden frame, and clearly tagged with alloy, Tempre, gauge, lapad, lot, net and gross weight and the eye direction (eye-to-sky or eye-to-wall).
Dry handling is essential because surface moisture would spoil the foil for printing and food contact.
Export is typically FOB, CFR or CIF, kasama 30% T/T deposit and balance against the bill of lading (L/C at sight for large orders).
The document set includes the bill of lading, commercial invoice, packing list, mill certificate and certificate of origin, plus food or pharma declarations and third-party inspection reports as required.
Full containers of jumbo rolls are the most economical for repeat converter business.
Eye direction is chosen for the converter’s handling: eye-to-sky rolls, with a horizontal axis and the core lifted by a shaft, suit shafted unwinders, while eye-to-wall rolls stand on their flanges for C-hook or forklift handling.
A 20- or 40-foot container is loaded by net weight, and pallet dimensions and roll OD are calculated to fill the container without crushing the outer layers.
Rolls should be stored indoors in dry conditions and off the floor, kept in their protective wrapping until use, and converted on a first-in-first-out basis to avoid long storage of light-gauge food foil.
Jumbo rolls are priced per tonne as the aluminum ingot price plus a processing fee.
The metal base follows the daily LME and the Shanghai futures and spot quotations, so quotations carry a validity window of a few days and are re-confirmed at deposit;
the processing fee reflects the rolling, pagsusubo, degreasing, surface, width and any slitting, and is lower for standard gauges and wide, full-width rolls than for unusual or very thin gauges.
Converters lower cost by standardizing gauges and widths, ordering full containers, and not over-specifying the gauge or surface.
Quotes far below market usually reflect a thinner actual gauge, a higher pinhole level, a cheaper alloy or missing documentation rather than a genuine advantage.
For converter buyers the metal itself is most of the cost, so the processing fee is the main commercial variable: it is lowest for standard-gauge, full-width, one-side-mill O stock and rises for double-zero light gauges, both-side bright, deep degreasing, narrow slitting and special cores.
Freight is meaningful for a dense metal product, so port choice, container loading and local import duty should be included when comparing a domestic converter with an imported jumbo roll.
A stable rolling forecast and a single specification per container typically secure the best repeat price.
For jumbo rolls the key distinction is an integrated foil mill that casts, mga rolyo, anneals, degreases and slits its own coil versus a trader that resells rolls.
A mill controls gauge, pinholes, surface and lot traceability and can match a converter’s line; a trader suits small, mixed orders.
China’s foil industry is concentrated in Henan, Shandong and the Yangtze and Pearl River deltas.
Verify the mill’s food/pharma production, the alloy and temper, lot certificates and migration reports, and always run production samples on your own lamination, slitting or pressing line.
During incoming inspection converters verify the coil tag against the paperwork, weigh the roll, measure width and core, and coupon-test gauge, wettability, tensile and elongation before committing the coil to a long run;
a short trial quantity is normal for a new mill or a new specification.
A capable mill supports this with stable lead times (commonly a few weeks for standard gauges), repeatable lots and responsive technical support,
And it will adjust the anneal or winding when a converter reports a runnability issue rather than simply reselling generic stock.
To start, contact Huawei with the gauge, lapad, core, Tempre, quantity and target market for a factory-direct quotation and production samples.
Henan Huawei Aluminum Co., Ltd (HWALU) is a privately owned aluminum manufacturer established in 2001, based in Huiguo Town, Gongyi, Henan—known as China’s Aluminum Capital, in the heart of the country’s aluminum rolling industry.
With around 1,200 employees including a specialist R&D team and a site of about 250,000 metro kuwadrado,
HWALU produces more than 200,000 tonnes of aluminum products a year and, as an integrated mill rather than a trader, mga rolyo, anneals,
degreases and slits its own foil for customers in more than 70 countries. Office: No.52, Daang Dongming, Zhengzhou, Henan, Tsina.
HWALU manufactures aluminum sheets, coils, mga foil, strips and circles across the 1000 sa 8000 serye, with food and pharmaceutical packaging foil among its core products.
We supply 8011 aluminum foil jumbo rolls (along with 1235, 8079, 8021 at 3003) for flexible packaging lamination, household-foil conversion, mga lalagyan ng pagkain, lidding, bottle caps and pharma lidding, in O temper with a clean degreased surface, controlled pinholes and consistent gauge.
Food-contact and pharma certificates, custom width and core, slitting, embossed or non-stick stock and moisture-proof export packing are available.
Email [email protected], or WhatsApp / call +86 18137782032 for a specification-based quotation and production samples.
A: It is the wide, large-diameter mother roll (parent roll) produced at the mill, sold by the tonne to converters who slit, laminate, print, coat or press it into finished products.
A: About 5.3–200 µm thick and 100–1600 mm wide, on 76 mm or 152 mm paper, steel or aluminum cores; light-gauge foil can be wider on request.
A: Its iron and silicon give tensile and puncture strength and fewer pinholes at light gauges, while the O temper is clean and easy to print, laminate, slit and form.
A: Gumamit 8011 for household foil, mga lalagyan, lids and most 9–30 µm barrier webs; use 1235 o 8079 for ultra-thin 6–9 µm laminated films.
A: Pinhole count, gauge and profile, flatness, degreasing and wettability, splice count, edge quality, winding tension and surface cleanliness, all tied to the lot certificate.
A: Yes—mill certificates with FDA, EU 1935/2004 and GB 4806 food-contact declarations, and pharma blister/lidding documents, are supplied for the specific lot.
A: Wrapped in moisture-proof film with end protectors on wooden pallets or in wooden frames, clearly tagged, and shipped by FOB/CFR/CIF with full export documents.
A: Per tonne as ingot price plus a processing fee, following the daily LME/Shanghai spot and re-confirmed at order; full containers are the most economical.
Ang 8011 aluminum foil jumbo roll is the converter-grade foundation of the food and pharmaceutical packaging industry.
Its iron-and-silicon chemistry delivers the strength, pinhole resistance and thin-gauge runnability that laminators, household-foil winders, container plants and lidding producers need, while the O temper provides a clean, degreased surface for printing and coating.
The specification follows the conversion: a 9–25 µm web for household foil and pouches, 40–200 µm for containers, 30–45 µm for lids, with the right core, lapad, splice and wettability grade.
Sourcing from an integrated mill that controls rolling, pagsusubo, pinholes and lot documentation gives converters the highest line efficiency and lowest landed cost.
Henan Huawei Aluminum Co., Ltd. ay ang pinuno ng maraming mga paggawa at mga supplier ng aluminyo sa China. Mahigpit naming kinokontrol ang kalidad at tumutok sa mga customer. Umaasa kaming magkaroon ng malalim na pakikipagtulungan sa iyo at mabigyan ka ng mataas na kalidad na mga produkto ng aluminum material na custom na serbisyo ng OEM. Kung gusto mong makuha ang pinakabago at pinakamahusay na mga presyo sa bawat kg o bawat toneladang karaniwang timbang, mangyaring makipag-ugnayan sa amin.