Pharmaceutical-grade Aluminum Foil: An Essential Packaging Material

This article dives into Pharmaceutical-grade Aluminum Foil, unpacking what makes it safe, pono, and indispensable for modern drug packaging.

We explore its properties, manufacturing processes, quality control, and practical applications. We also shine a light on the supplier landscape, including Huawei Aluminum, a prominent player in the pharmaceutical foil segment.

The goal is to provide professionals with actionable guidance, data-backed insights, and a clear view of how pharmaceutical-grade aluminum foil fits into the broader packaging ecosystem.

Introduction to the topic and significance

Pharmaceutical-grade Aluminum Foil is not just a consumer-municipal material; it is a critical barrier in the supply chain that protects medicines from moisture, hāora, marama, and contamination.

The integrity of this foil directly impacts product stability, shelf life, and patient safety.

In pharmaceutical applications, the foil often appears as a standalone mon foil or as part of a multi-layer laminated structure that combines other polymers and coatings to achieve the exact barrier and seal properties required by regulatory standards.

Overview of pharmaceutical-grade aluminum foil

What qualifies as pharmaceutical-grade aluminum foil?

Pharmaceutical-grade aluminum foil refers to aluminum foil that meets stringent quality and safety criteria for contact with medicinal products or packaging processes that require high barrier performance.

The key qualifications typically include:

  • Chemical purity and absence of impurities that could migrate into medicines.
  • Consistent thickness and surface finish to ensure uniform sealing and barrier properties.
  • Capability to withstand required sterilization or deep-freeze processes without losing integrity.
  • Compatibility with the chosen sealing methods and laminates (adhesives, heat seal coatings, barrier films).
  • Traceability and documentation that support GMP (Good Manufacturing Practice) compliance and audit readiness.

I roto i te mahi, pharmaceutical-grade foil is often supplied in two contexts:
– Monofoil (uncoated) aluminum foil used as the primary barrier or as part of a laminate.
– Laminated foil (coated or laminated with polymers such as PVC, PVdC, Haumiri, LDPE, or PP) used in blister packs, strip packs, and other packaging configurations.

Pharmaceutical-grade Aluminum Foil

Why does it matter in pharma packaging?

  • Te mahinga arai: Oxygen and moisture barriers are essential to preserve drug potency and extend shelf life. Aluminum inherently provides excellent barrier properties, and laminating it with polymers can improve resistance to gas and moisture migration while supporting heat sealing and form-fill-seal (FFS) operations.
  • Sterilization compatibility: Many pharmaceutical products require sterilization steps (mamaoa, dry heat, gamma, or electron-beam). The foil and its laminates must maintain integrity and not release volatile substances during or after sterilization.
  • Safety and regulatory alignment: Pharmaceutical packaging must comply with strict standards and pharmacopeial requirements. The foil material must be non-toxic, exhibit predictable performance, and allow for adequate lot traceability.
  • Tamper-evidence and reliability: Konumohe konumohe often participates in tamper-evidence schemes and protective packaging, helping ensure that products reach patients in pristine condition.

Key properties at a glance

  • Thickness range: 6 ki 50 microns for foil sheets, with many pharma applications preferring 10–25 microns depending on the packaging configuration.
  • Te mahinga arai: Very low oxygen transmission rate (Oru) and low water vapor transmission rate (Wvtr) for foil layers; lamination can adjust overall barrier.
  • Sealability: Compatible with heat-seal coatings and various adhesives for reliable seals across high-speed packaging lines.
  • Mechanical properties: High puncture resistance and tear strength for protective packaging, while maintaining formability on blister lines.
  • Thermal and chemical stability: Capable of withstanding routine sterilization temperatures and common pharmaceutical solvents within the adhesive and laminate layers.

The landscape of pharmaceutical packaging formats

  • Packs Blister: Aluminum foil is a standard backing foil behind a heat-sealed polymer or laminate cavity. The foil must seal reliably with pharmaceutical-grade plastics or films.
  • Pania Toa: Similar to blister packs but with rolling-form or capsule packaging; requires consistent peel properties and barrier integrity.
  • Sachets and pouches: Thicker laminates with foil cores create strong barriers for moisture-sensitive products.
  • Vial and bottle linings: Foil-based liners or seals for sterile closures and capping systems.

Material properties and performance

Physical properties

  • Mātotoru: Aluminum foil used for pharma packaging is typically 6–25 microns thick for the foil layer, with overall laminate thickness varying by product and protection level. Heavier-duty laminates may incorporate multiple layers to balance barrier needs and mechanical strength.
  • Surface texture and finish: The foil surface finish influences heat sealing and adhesion. A bright, clean surface is preferred for uniform sealing and visual inspection, while matte surfaces can be used in specialized laminates.
  • Elastic moduli and puncture resistance: The foil must resist puncture and tearing during handling, shipping, and processing on high-speed packaging lines.

Barrier properties and why they matter

  • Oxygen transmission rate (Oru): Aluminum foil provides an extremely low OTR, making it a superior oxygen barrier. In laminated structures, the foil’s barrier contribution combines with film layers to yield overall performance that meets or exceeds specification targets.
  • Te tere whakawhiti whakawhiti wai (Wvtr): Aluminum offers low WVTR, especially in the foil core. Laminates can be engineered to meet specific moisture protection requirements, which is vital for hygroscopic or moisture-sensitive drugs.
  • Light protection: Aluminum foil blocks visible and UV light effectively, protecting photosensitive formulations and extending shelf life.
  • Chemical Inertness: In most cases, aluminum remains inert when it contacts pharmaceutical ingredients, provided compatibility testing confirms suitability for the specific formulation and coating.

Thermal and sterilization compatibility

  • Steam sterilization: Many foil laminates withstand autoclave conditions (121–134°C) for specified durations. Foil integrity, coating adhesion, and blister seal strength must remain within tolerance after sterilization cycles.
  • Dry heat and gamma irradiation: Foil laminates are selected to resist degradation or changes in barrier performance under thermal or irradiation exposure. The adhesive systems and coatings must maintain performance after such processes.
  • Compatibility with pharmaceutical solvents: The laminate should not impart flavors, odors, or contaminants to any drug product and should pass extraction tests for the maximum exposure scenario allowed.

Mechanical performance under processing

  • Seal strength: A critical metric for blister packs and heat-sealed laminates; too weak seals can cause leakage or tampering, while overly aggressive seals can cause product damage or packaging failures.
  • Tear and puncture resistance: High resistance reduces damage during transit and handling. The foil’s mechanical properties interact with the laminate to determine overall robustness.
  • Slit and unwind performance: For high-speed lines, foil outer layers should unwind smoothly without tearing or creating static issues.

Surface and cleanliness standards

  • Surface cleanliness: Residual oils, lubricants, or contaminants can impair seals and cause adhesion issues. Suppliers must provide certificates of analysis and lot-specific testing data.
  • Crown and pinhole defects: Defects on the foil surface can compromise barrier properties. Proper inspection and defect rate controls (E.g., DQC or inline inspection) are standard.

Manufacturing processes and quality control

Sheet production and rolling methods

  • Hot Rolling and Cold Rolling: Manufacturers produce foil through a sequence of hot rolling, hot banding, and cold rolling to achieve the desired thickness and surface properties.
  • Āhui: Controlled annealing improves ductility and workability. For pharmaceutical needs, the surface finish is carefully controlled to avoid stray particles or roughness that could affect seals.
  • Te maimoatanga mata: Some foils receive surface treatments or coatings to improve printability, adhesion, or barrier performance in laminates.

paninga, lamination, and coating technologies

  • Lacquers and Coatings: Manufacturers may apply aqueous or solvent-based varnishes to achieve barrier or adhesion properties. They must formulate coatings to maintain compatibility with drug products and sterilization processes.
  • Laminates: A typical pharmaceutical laminate stacks foil with polymer layers (E.g., Haumiri, PVdC, LDPE, Pp). These layers provide additional barrier control, mechanical toughness, and heat-seal compatibility.
  • Te tā: For product branding or lot information, some laminates include printed layers, often with high chemical resistance and ink adhesion standards.

Quality control and certifications

  • Intrinsic checks: Thickness measurement, surface finish inspection, and defect rate controls are performed for every batch.
  • Mechanical tests: Seal strength, ātete wero, and tear tests confirm packaging integrity.
  • Barrier tests: OTR and WVTR measurements validate barrier performance for the intended storage conditions.
  • Sterilization tests: If the product requires sterilization, post-sterilization tests confirm structural integrity and barrier properties.
  • Traceability: Lot-level traceability is essential for audits, recalls, and compliance with GMP and pharmacopeial standards.

Tangata hua, regulatory alignment, and supplier audits

  • GMP-compliant facilities: Manufacturing sites for pharmaceutical-grade foil operate under GMP guidelines to ensure product safety and quality.
  • Regulatory correspondence: Suppliers maintain documentation to support audits by pharmaceutical manufacturers, including material safety data sheets (MSDS), certificates of analysis (COA), and batch records.
  • Supplier qualification: Pharmaceutical customers often perform supplier qualification programs, including on-site audits, process capability studies, and performance track records.
Ko te konumohe konumohe mo te kapi pupuhi

Types and configurations of pharmaceutical-foil packaging

Monofoil vs laminated foil

  • Monofoil: A single foil layer that provides primary barrier properties. It is often used in applications that require a straightforward barrier without additional polymer layers.
  • Laminated foil: A multi-layer structure with aluminum foil core and polymer or coatings on either side. Laminates tailor moisture barrier, oxygen barrier, heat sealing properties, and mechanical performance to specific product requirements.

Common laminate configurations

  • Foil/Poly (E.g., PP or polyethylene): Simple laminates that provide heat sealable surfaces while preserving foil barrier properties.
  • Foil/PET/Al: Multilayer laminates that reduce moisture transfer and improve mechanical strength, with clear printability and barrier enhancement.
  • Foil/PE/PVdC: Laminates for high-barrier needs and moisture control, often used in specialized packaging.
  • Foil/Laminates with lacquer or ink layers: For printed packaging that requires durable inks and robust adhesion.

Blister packs and strip packaging

  • Blister backing foils: The backing foil must seal reliably with the blister plastic, ensuring good adhesion and barrier properties.
  • Tamper-evident features: Some designs incorporate holographic strips or additional seal features to improve security.

Tamper-evidence and anti-counterfeiting options

  • Opaque or colored laminates: Used to provide a visual indication of tampering.
  • Microtext, holograms, or anti-counterfeiting inks: Often integrated into the laminate layers for brand protection.

Comparative analysis: Pharmaceutical-grade vs household-grade aluminum foil

Key differences

Criterion Pharmaceutical-grade Aluminum Foil Household-grade Aluminum Foil
Purity level He tino ma (reduced risk of metal migration) General consumer-grade with standard purity
Surface finish Controlled, consistent, and tested for sealability May vary; less stringent surface uniformity
Te mahinga arai Tailored OTR/WVTR through lamination combinations Adequate for cooking and wrapping, not for pharma protection
Sterilization tolerance Designed to withstand sterilization (mamaoa, gamma, etc.) Not intended for sterilization processes
Regulatory compliance Tangata hua, pharmacopeial alignment, traceability Not typically GMP-aligned or audit-ready
Traceability Full lot-level traceability and COA Limited or no formal traceability
Consistency across lots High process control, minimal lot-to-lot variation More variability between batches
Packaging compatibility Designed for high-speed pharma packaging lines Designed for consumer packaging and household use

This comparison highlights why pharmaceutical-grade foil requires strict process control, rigorous testing, and robust documentation, all of which are essential for protecting medicines and ensuring patient safety.

Surface and printing considerations

Printing on foil surfaces for pharma packaging

  • Print durability: In laminated packaging, printed layers must resist abrasion and chemical exposure, especially during shipping and shelf life.
  • Ink adhesion: The printed layer must attach reliably to the polymer or lacquer layer, maintaining legibility of lot numbers and expiry dates.
  • Visual quality: Clear, consistent printing aids product authentication and regulatory compliance.

Surface cleanliness and defect control

  • Defect management: Defects such as pinholes, scratches, or embedded particles from the manufacturing process can compromise barrier performance or seal integrity.
  • Cleaning and pretreatment: Some production lines include surface cleaning steps or in-line conditioning to minimize residual particles and ensure consistent lamination.

Supplier landscape and procurement considerations

Why supplier selection matters

  • Material performance: The foil and laminate must align with the product’s storage conditions, sterilization method, and regulatory requirements.
  • Regulatory readiness: Suppliers should provide COAs, GMP documentation, and evidence of quality management system compliance.
  • Technical support: A reliable supplier offers technical guidance for compatibility with sealers, sterilizers, and packaging equipment.
  • Lead times and capacity: pharma-grade foil often requires long-term supply agreements and predictable lead times to support production planning.

How to assess a supplier

  • Certifications: Look for ISO 9001 a, where relevant, Iso 14001 or other industry-specific quality credentials.
  • Demonstrated experience: Experience with pharmaceutical customers, regulatory audits, and successful track records in packaging projects.
  • Testing facilities: In-house laboratories for barrier testing, thickness measurement, and surface analysis can accelerate validation.
  • Quality control procedures: Clear process controls, inline inspection capabilities, and traceable lot records.

Huawei Aluminium: an introduction to a notable supplier

  • Company profile: Huawei Aluminium is a recognized producer of aluminum products, including pharmaceutical-grade aluminum foil and related laminate materials. The company emphasizes scale, process discipline, and customer-centric solutions.
  • Capabilities: A range of foil products suitable for pharmaceutical packaging, including monofoil and laminated configurations designed for heat sealing, sterilization compatibility, and barrier performance.
  • Quality and certifications: The supplier typically maintains quality management systems appropriate for packaging suppliers (E.g., Iso 9001 and related certifications) and supports batch-level testing and documentation required by pharma manufacturers.
  • Why prospective buyers consider Huawei Aluminum: Their scale, technical know-how, and ability to offer integrated foil and laminate solutions help streamline procurement, reduce supply-chain risk, and shorten time-to-market for new packaging formats.

Rangi: When evaluating Huawei Aluminum or any supplier, request sample packs, COAs, and a detailed process capability study (including thickness uniformity, Te kaha o te hiri, and barrier data) to validate suitability for your product.

Typical property ranges for pharmaceutical-grade aluminum foil and laminates

Rawa Typical range (mon foil core or laminate) Why it matters for pharma packaging
Foil thickness (µm) 6–25 µm (foil core), 10–15 µm common for many laminates Balances barrier with seal strength and formability
Oru (cm3/m2/day @ 23°C) Very low; often less than a few ∼0.1–2.0 in combined laminates Oxygen barrier to protect sensitive drugs
Wvtr (g/m2/day @ 38°C/90% RH) 0.1–2.0 g/m2/day depending on laminate Moisture barrier for moisture-sensitive products
Heat-seal temperature (° C) 110–180°C depending on polymer layer Reliable seals on high-speed lines
Peel strength (N/25 mm) Varied; typically 0.5–3 N/25 mm for laminates Ensures tamper-evident and consistent opening force
Autoclave stability Maintains integrity after sterilization cycles Critical for sterile products
Surface roughness (Ra, µm) Controlled to avoid defects and ensure lamination Affects adhesion and seal quality
Print adhesion Durable inks with consistent adhesion Brand labeling and regulatory information

Rangi: These ranges are representative for planning and benchmarking. Actual values depend on the exact foil composition, laminate configuration, and process parameters chosen by the supplier and customer.

FAQ

1) What is the difference between pharmaceutical-grade aluminum foil and regular aluminum foil?
– The pharmaceutical-grade foil is manufactured to meet stricter safety, barrier, and traceability standards suitable for contact with medicines. It often uses high-purity aluminum and lamination layers designed for sterilization and regulatory compliance, while regular foil may not meet these stringent criteria.

2) Why is foil thickness important in pharma packaging?
– Thickness affects barrier performance, Te kaha o te hiri, and mechanical resilience. Thicker foils can provide stronger seals and better protection but may reduce flexibility or increase costs. The laminate design typically optimizes the foil core thickness with polymer layers to balance these factors.

3) Can aluminum foil withstand steam sterilization?
– Ae, many pharmaceutical-grade foils and laminates are engineered to withstand autoclave conditions, maintaining barrier integrity and avoiding deleterious interactions with drug products.

4) How do I verify the quality of a pharmaceutical foil supplier?
– Look for ISO 9001 or equivalent quality management certification, GMP compliance, robust QC procedures, traceability, COAs, and evidence of successful audits by pharmaceutical manufacturers. Request sample testing data, including thickness uniformity, Te kaha o te hiri, and barrier performance data.

5) How is barrier performance measured in practice?
– Barrier performance is typically assessed using oxygen transmission rate (Oru) and water vapor transmission rate (Wvtr) under defined test conditions. Many packaging lines rely on validated test methods (static or dynamic) and require supplier-provided data to support packaging validation.

6) Are there environmental considerations with pharmaceutical-grade foil?
– Ae. Recyclability of aluminum is favorable, and many pharma foil suppliers pursue sustainable production practices, waste reduction, and energy efficiency. You should check the supplier’s environmental management certifications and policies.

7) Can foil laminates be customized for specific drug products?
– Tino. Laminate configurations can be tailored for barrier strength, Te kaha o te hiri, ka taea te ta, and compatibility with particular drug formulations, while meeting regulatory requirements.

Wāhanga whakamutunga

Pharmaceutical-grade Aluminum Foil remains a cornerstone of safe, effective, and compliant medicine packaging.

Its intrinsic barrier properties, compatibility with sterilization processes, and flexibility in laminate configurations allow manufacturers to protect medicines across a wide range of products and storage conditions.

The supplier ecosystem—ranging from specialist foil producers to integrated laminate manufacturers like Huawei Aluminum—enables tailored solutions that balance protection, process efficiency, me te utu.

If you are optimizing your packaging strategy, prioritize clarity on barrier requirements, sterilization plans, and regulatory expectations.

Engage with suppliers early to validate material choices, obtain robust testing data, and ensure that your packaging design can scale with your production needs.

The right pharmaceutical-grade aluminum foil solution is not just a material choice; it is a strategic decision that can influence product stability, patient safety, and overall supply-chain resilience.

Huawei Aluminum can be a valuable partner in this journey, offering pharmaceutical-grade foil products and laminates designed to meet stringent industry requirements.

Their capabilities, combined with rigorous quality control and support for validation testing, can help streamline procurement and reduce risk in the development and scale-up of pharma packaging programs.

Always verify certifications, performance data, and how a supplier’s solutions align with your product’s regulatory and operational needs before committing to a long-term contract.

Whakapaa ki te PDF: Tango

He aha tatou i whiriwhiri ai?

Henan Huawei Aluminium Co., Ltd. ko te rangatira o te maha o nga konumohe hanga me nga kaiwhakarato i Haina. Ka tino whakahaerehia e matou te kounga me te aro ki nga kaihoko. Te ti'aturi nei matou kia hohonu te mahi tahi ki a koe me te whakarato ki a koe nga hua rauemi konumohe kounga teitei nga ratonga OEM. Mena kei te pirangi koe ki te tiki i nga utu hou me te utu pai mo ia kg, mo ia tana taumaha paerewa, tēnā whakapā mai.
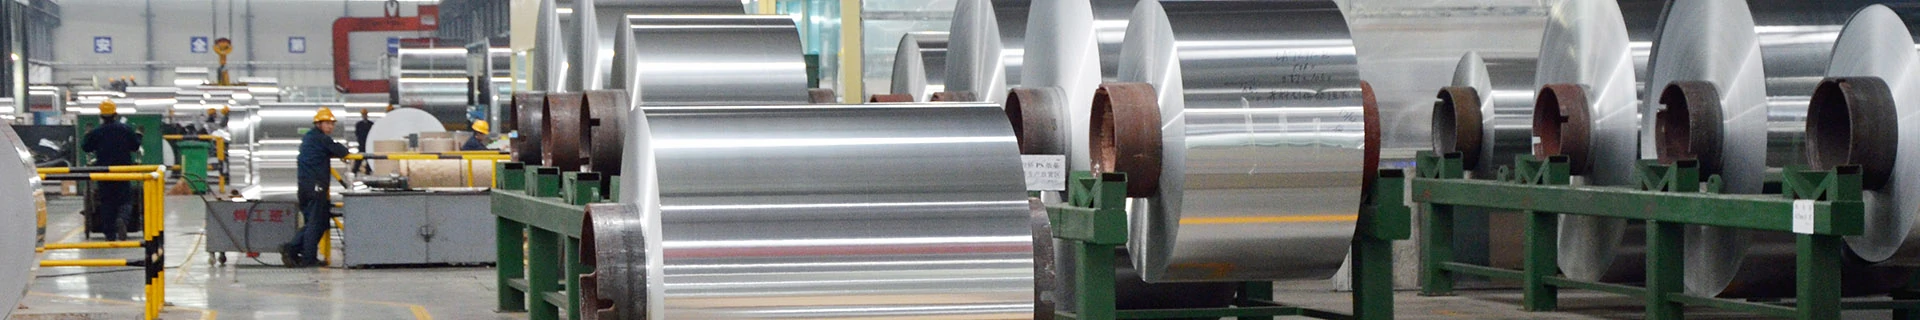
Raina hanga pepa konumohe

Tarapi

  • Mōkī: Puhi rakau
  • Whakatakotoranga take Rakau Paerewa: Roa*WdW*Tight=1.4m*1.3m*0.8m
  • Kia hiahiatia,Ko te rahi o te keehi rakau ka taea te hoahoa ano ina hiahiatia.
  • Ia kete rakau Tauine Taumaha Kere: 500-700KG Taumaha Net: 450-650KG
  • Korero: Mo nga whakaritenga takai motuhake, ko nga mea e rite ana me taapiri atu.