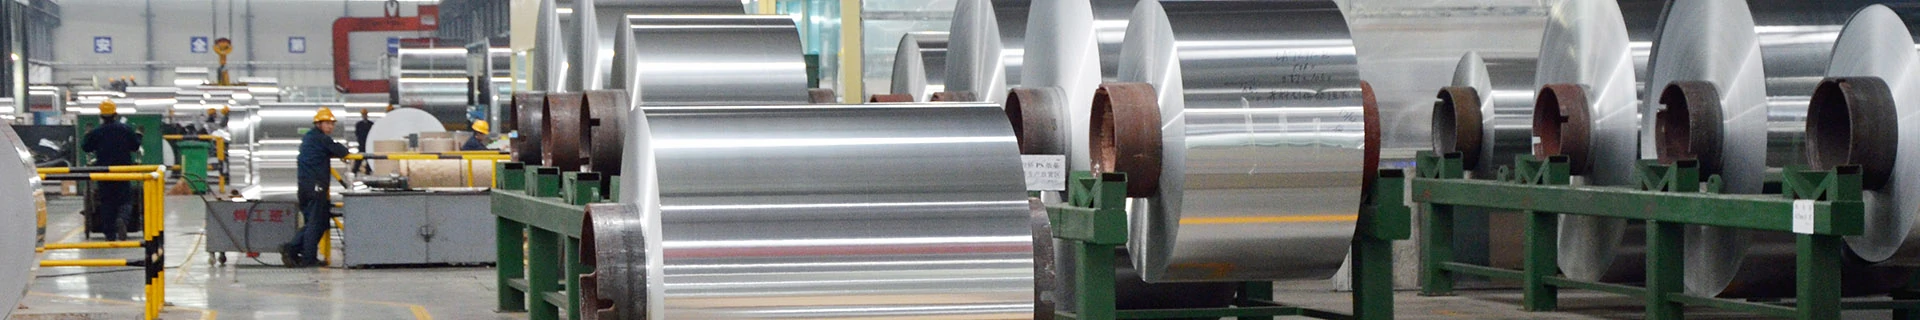
А 1235 O raw material aluminum foil is a soft, fully annealed, unprinted foil supplied as a master or slit roll. In other words, it is the bare metal web that downstream converters buy before they laminate, print, emboss or coat it.
The letter O tells us that the foil is fully annealed and therefore soft.
This distinction matters because raw foil is not a finished package. Первый, it carries no heat-seal layer of its own. Следующий, it has no printed outer face. Окончательно, it is wound as a continuous web that must run cleanly on the customer’s own equipment.
Следовательно, the quality of this starting material sets the ceiling for every later process.
This guide explains how the raw foil is produced, how the soft O temper is achieved, and which properties a buyer should inspect.
It also covers pinholes, поверхностная чистота, winding quality and the documents that accompany each batch. A related technical view is available on our 1235 aluminum foil as the core layer in food composite films page.
Quick specification overview for 1235 O raw material aluminum foil
To begin with, the term raw material describes the position of the product in the supply chain. The rolling mill produces a thin metal web, and that web is then sold to a converter.
The converter adds the polymer, paper or coating and turns the metal into a finished packaging film. In this relationship, the bare foil is the input rather than the end product.
By contrast, a finished laminated film already contains several layers. Например, a PET/AL/PE web can be printed and heat-sealed without further conversion.
The raw foil, однако, cannot do either job on its own. Следовательно, buyers who only need the metal web should order raw stock, while those who want a ready-to-run pack should order a finished laminate.
На практике, many converters prefer to buy raw foil because they already control the adhesive and printing. This division lets each party focus on its own strength.
The mill supplies a consistent metal web, and the converter applies its own converting know-how.
Кроме того, the order can be placed at two widths. A master roll is the wide web produced directly by the mill, while a slit roll has been cut to the narrow width the converter runs.
Some large converters buy master rolls and slit them in house, whereas smaller plants prefer ready slit widths. In either case, the metal itself is the same 1235 O raw material aluminum foil, and the choice only reflects how the customer handles the web.
Сплав 1235 belongs to the 1xxx series of industrial pure aluminum. Its aluminum content is at least 99.35 percent, and the remaining iron and silicon are each held below about 0.6 percent.
That tight composition gives the foil its softness and its clean, bright surface.
For raw stock, high purity is a practical advantage rather than a marketing detail. Первый, a pure web is ductile and tolerates repeated folding.
Следующий, it produces fewer pinholes at a given gauge. Окончательно, its bright face supports later printing and embossing. These traits explain why 1235 is a common starting material for flexible packaging.
The O temper means the foil is fully annealed after rolling. During annealing, the work-hardened metal is softened and its internal stress is released.
Следовательно, the web lies flat, forms easily and bonds well with later adhesives. For most flexible conversion, O is the default temper.
On the mechanical side, the soft web typically shows a tensile strength around sixty to eighty megapascals and an elongation above twenty percent.
These figures vary with gauge, so the exact values should always be read from the mill test certificate rather than treated as fixed. На практике, a soft foil is not chosen for raw strength.
Вместо, its value lies in elongation and the way it survives forming without cracking.
The production route begins with melting and casting. The aluminum is alloyed to the 1235 composition, filtered for cleanliness and cast into a thick slab or a continuous cast coil.
Кроме того, hydrogen and non-metallic inclusions are removed at this stage because they would later become defects in the thin foil.
The cast coil then passes through a series of cold rolling passes, and each pass reduces the gauge. As the metal approaches foil thickness, the work moves to a dedicated foil rolling mill.
At this point, two webs are often rolled together, which produces the familiar bright and matt faces.
After rolling, the hard web is loaded into an annealing furnace and heated under a controlled cycle. The heat softens the metal, removes residual rolling oil and relieves the stress built up during reduction.
Как результат, the foil exits in the soft O temper and is ready for slitting.
The annealing cycle must be balanced carefully. Например, insufficient heating leaves the foil hard and oily, while excessive heating can coarsen the surface.
Следовательно, the furnace temperature and dwell time are set against the gauge and the final application.
At the final foil pass, the mill often doubles two webs and rolls them together. The faces that touch the polished rolls become bright, while the faces that touch one another stay matt.
This is why a single foil can show two different finishes. After rolling, the webs are separated and annealed. The doubling step also helps the mill reach very thin gauges that would be difficult to control as a single web.
Once the foil is soft, its dimensional quality becomes the main concern. A tight gauge tolerance keeps tension stable on high-speed lines, and good flatness prevents wrinkles during conversion.
Even a small thickness variation can force the converter to slow the machine or reject the web.
Pinholes are tiny through-thickness holes that act as leak paths, and they are the natural enemy of a barrier foil. As the gauge drops, pinholes become more difficult to avoid.
Следовательно, standards grade the allowed count according to thickness rather than applying one fixed limit.
Стол 1. Typical pinhole grading by nominal foil thickness
На практике, a slightly thicker foil with zero pinholes often outperforms a thinner web that saves metal but leaks.
Следовательно, buyers should specify the pinhole requirement together with the gauge rather than treating the two separately.
Pinhole inspection is not a one-off check at the end of the order. Вместо, samples are taken at set intervals across the batch and examined over a light source.
If a sample exceeds the agreed limit, the surrounding length is quarantined and reviewed rather than shipped. This routine protects the converter because a hidden pinhole only becomes visible after the barrier has failed in service.
The foil surface must be clean because even a thin film of rolling oil can stop the later adhesive from gripping.
The annealing cycle removes most of this oil, and the finished web is then checked for a dry, uniform face. Кроме того, the surface should be free of stains, bright lines and corrosion marks.
Wetting tension is the practical measure of this cleanliness. A higher tension lets the adhesive spread into a continuous film instead of pulling back into droplets.
If the tension is too low, the converter may need an extra corona or plasma treatment before bonding. Следовательно, a clean, high-tension surface saves a downstream step.
For this reason, the mill and the converter should agree on a minimum wetting figure at the order stage. When the incoming foil already meets that figure, the first laminating run is far more predictable.
Several surface defects are explicitly excluded from a sound raw web. Например, inclusions, царапины, морщины, cracks and overlapping edges must not appear across the usable area.
The same rule covers rolled-in debris and uneven color. A clean surface is not only an appearance issue. Each defect can become a starting point for a tear, a leak or a weak bond during later conversion.
A raw foil roll is only usable if it winds and unwinds without incident. The edges must be clean and aligned, the core must hold its dimension, and any splices must be marked and limited.
A single damaged edge can telescope the roll or cause a web break on a high-speed line.
Slitting is the step that turns a wide master roll into the customer’s requested widths. Tight blade control prevents burrs and edge dust, and consistent winding tension keeps the roll firm.
Тем временем, splices are kept to an agreed number and flagged so the converter can prepare for them.
The core inner diameter is normally 76 или же 152 миллиметры, and it must match the customer’s unwind shaft. A stable core prevents the roll from slipping or collapsing.
These details look minor, yet they directly determine how smoothly the web runs.
Winding tension is controlled across the full roll so the web stays firm without being crushed. A roll wound too loosely can telescope when handled, while one wound too tightly can damage the soft edges.
The converter should also respect the shelf condition of the foil and use the oldest batch first. When rolls are kept sealed and dry, the surface retains its wetting quality until conversion.
A disciplined buyer does not accept raw foil on appearance alone. Первый, the mill test certificate is checked against the order. Следующий, samples are taken from the delivered batch and measured.
Окончательно, a first article is run on the real converting line before the bulk is released.
Стол 2. Raw material inspection items and how they are checked
The value of this routine is early detection. A defect found at incoming inspection is cheap to resolve, whereas the same defect found after printing or lamination has already consumed added work.
Следовательно, the inspection should happen before the foil enters production.
The sampling plan should be agreed in writing so both parties judge the batch against the same rule. A practical approach selects samples from the start, middle and end of a roll rather than from one convenient point. Кроме того, any measured value is compared with the MTC and the agreed tolerance. When a result sits outside the limit, the batch is held for investigation instead of being released by assumption.
The same soft raw foil can feed several converting routes, and each route stresses a slightly different property.
Our technical note on 1235 aluminum foil composite flexible packaging explains how the soft web forms a stable bond when the surface is correctly prepared.
That same principle applies whether the next step is lamination, coating or printing.
When the specification is agreed with the final process in mind, the converter avoids repeated adjustments. На практике, stating the gauge, характер, wetting figure and splice limit together is more useful than ordering a generic foil.
Although the foil is supplied as raw material, it is destined for a wide set of finished products. The six sectors below show where the soft 1235 web is commonly converted.
Первый, flexible food packaging uses the web as the barrier core of pouches and sachets. Второй, retort and lidding rely on its heat tolerance, a family covered on our 8011 aluminum foil for dairy packaging page.
Third, cigarette and label work values its bright, printable face.
Fourth, cable and insulation converters laminate the foil for shielding. Fifth, батарея, capacitor and tape applications use its clean, consistent surface.
Sixth, pharmaceutical blister webs apply the same barrier logic, as shown on the PTP blister aluminum foil page.
Стол 3. Full specification, packing and storage summary
Because the foil is soft and unprotected, packing and storage are part of the product rather than an afterthought. Moisture at the edge can weaken later bonds, and a crushed roll can ruin the winding.
Следовательно, rolls are sealed in a moisture barrier and kept dry until conversion.
Хэнань Huawei Aluminium Co., ООО. is an aluminum foil manufacturer based in the Gongyi aluminum cluster in Henan, Китай.
The company was founded in 2001 and runs integrated rolling, отделка, slitting and annealing capacity for soft foil.
The site covers roughly 250,000 square meters with about 1,200 people and an annual capacity of more than 200,000 тонны.
The foil is exported to more than seventy countries, so the packing and documentation follow international practice.
For raw material buyers, HWALU can supply 1235 in the soft O temper with custom gauge, ширина, core and surface requirement.
Each batch is supported by a mill test certificate and traceable batch marks, and the technical team reviews the specification before production. That consistency is what makes long-term repeat supply reliable.
Each batch of 1235 O raw material aluminum foil is given a clear batch mark, and that mark links the physical roll to its chemistry, gauge and mechanical results.
The buyer can therefore trace any delivered roll back to the exact production run. This traceability is especially useful when a converter qualifies a new product, because later shipments can be compared directly with the approved first sample.
Q: Is this a finished film or a bare raw material?
А: It is a bare, unprinted 1235 foil supplied as a master or slit roll. Downstream converters add the polymer, coating or print, so the metal is the starting material rather than a finished package.
Q: What does the O temper mean?
А: O means the foil is fully annealed after rolling, which makes it soft and ductile. The annealing also removes residual oil and stress, so the web forms and bonds well.
Q: Which thickness and width are available?
А: The common range is 0.006 к 0.2 миллиметры, with six to thirty microns most used, and widths run from about 100 к 1700 миллиметры. Exact figures are slit to the order.
Q: How are pinholes controlled?
А: Pinholes are graded by thickness and checked with backlight inspection. Thicker gauges can reach zero pinholes, while thin gauges rely on tight process control and an agreed limit.
Q: Why is wetting tension specified?
А: Wetting tension shows whether the surface is clean and bondable. A high enough figure lets adhesive spread evenly and can remove the need for extra treatment at the converter.
Q: Which documents come with each batch?
А: A mill test certificate, packing list, commercial invoice and traceable batch marks are provided, with additional test reports available when the application requires them.
Общий, 1235 O raw material aluminum foil is the soft, clean metal web that sits at the start of the converting chain.
The purity sets the surface quality, the annealing sets the soft temper, and the gauge and pinhole control set the barrier.
Choosing the right raw stock means agreeing the gauge, терпимость, wetting figure, winding quality and documents before the first run.
Buyers who inspect at incoming stage and keep traceable batch records remove most of the avoidable risk.
In the end, a consistent raw foil is what allows every later process to run at high speed.
When the starting material is stable, the converter can print, laminate, emboss and coat with confidence and deliver a reliable finished product.