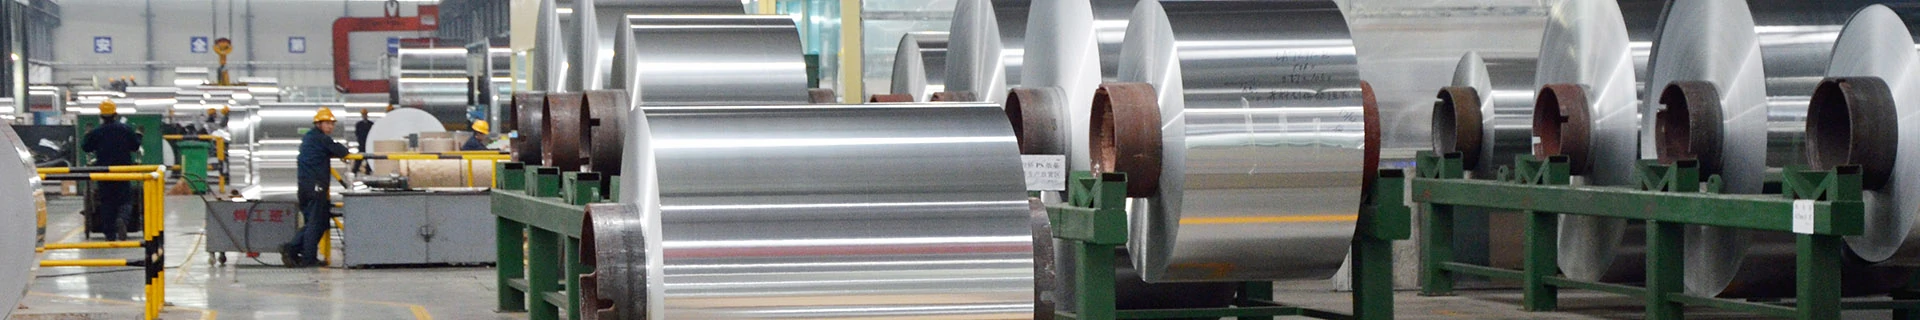
Food grade 3003 aluminum foil jumbo roll is the wide, large-diameter mother roll of Al-Mn alloy aluminum foil that converters slit, laminate, print, coat or press into food packaging.
Compared with the pure 1xxx and the 8xxx household foil grades, 3003 contains about 1.0–1.5% manganese, which raises strength, stiffness and corrosion (rust) resistance.
That makes 3003 the preferred food foil where the web needs body, temper and durability—formed food containers, cup lidding, bottle-cap stock, stiff lids, baking and roasting trays, and laminated barrier structures that must withstand processing.
A jumbo roll is not a retail product; it is the converter’s raw material. It is produced wide and heavy at the mill, sold by the tonne, and then converted downstream into household rolls, container webs, lidding rolls or printed laminates.
This guide explains what makes 3003 different from 8011 og 1235, the tempers and gauges used for food contact, the main food applications, food-safety compliance, quality control, pricing and ordering, and a core specification table.
It is written for foil converters, packaging producers, container factories and distributors.
Aluminum foil is rolled aluminum thinner than about 0.2 mm. De 3003 grade is a 3xxx-series Al-Mn alloy: manganese is the main addition, giving solid-solution strengthening and improved corrosion resistance compared with pure aluminum.
A jumbo roll (also called a parent or mother roll) is the wide, large-diameter roll produced at the rolling mill before slitting, typically 100–1600 mm wide and weighing hundreds of kilograms to tonnes, wound on a 76 mm or 150/152 mm core.
“Food grade” means the foil is produced from controlled stock, rolled and annealed without harmful lubricants or residues, degreased to a food-safe surface, and proven to meet food-contact regulations such as the US FDA,
EU -regulering (Ec) 1935/2004 og 10/2011, German LFGB, and China GB 4806.9. It must be non-toxic, tasteless and odorless. The alloy itself (3003) is a separate choice—food compliance is the cleanliness and certification of the production route.
This article focuses on 3003 aluminiumsfolie as a food packaging foil; the more common household grade is covered under 8011 aluminiumsfolie.
The typical 3003 chemistry is about 1.0–1.5% manganese, with small iron and silicon and the balance aluminum, as shown below.
Manganese is the strengthening element; it does not make the foil non-food-contact, and the alloy has a long history in packaging and kitchen foil.
The trade-off is that 3003 is slightly stiffer and more expensive than pure 1xxx or soft 8011, and it is not the best choice for ultra-thin household wrap.
But where the food packaging must be formed, sealed, handled and kept rigid—container webs, lidding, Hætter, baking trays—3003’s strength and rust resistance pay for themselves in fewer split or soft, wrinkled parts.
The reason aluminum foil is such a universal food barrier is that it is a fully dense metal: a continuous foil of even a few microns stops light, ilt, vanddamp, fedt, oil and odors completely, unlike plastic films that are only partial barriers.
This is why foil is the inner barrier in long-shelf-life foods, and why pinholes are the one defect that matters—a hole in the foil breaks the barrier.
3003 adds strength to that barrier without losing the metal’s blocking power.
8011 remains the workhorse of household foil and many semi-rigid food containers because its Fe/Si balance gives strength and pinhole resistance while staying soft and cheap.
1235 is used for ultra-thin laminated barrier webs. 3003 steps in where extra strength, stiffness and corrosion resistance matter:
formed container webs that must hold their shape, cup lidding that must peel cleanly and reseal, bottle-cap stock, and baking/roasting foil that sees heat and moisture.
Converters often run 8011 for soft wrap and 3003 for the stiffer, more demanding food parts.
For semi-rigid food container webs many customers compare 8011 foil for food containers med 3003;
for ultra-thin laminate barriers the choice is usually 1235 foil for flexible packaging.
A practical way to choose is by the job: if the web is simply wrapping, soft and cheap, 8011 O is the default.
If the web is deep-drawn into a tray, die-cut into a lid or cap, or exposed to heat and acidic food, 3003’s stiffness and rust resistance reduce breakage and rejected parts.
Many converters run both—8011 for soft household and light-container webs and 3003 for the stiffer, higher-performance food components—so ordering from a mill that makes both avoids switching suppliers.
3003 food foil is supplied mainly in O (annealed, blød) or H14/H24 (work-hardened and stabilized, half-hard) tempers.
O-temper 3003 is soft and formable, ideal for deep forming, baking trays and wrap where the foil must bend and draw without cracking.
H14/H24 gives a stiffer, stærkere, more dimensionally stable web, used for lidding that must stay flat, bottle-cap stock, and container edges that need stiffness.
The temper is chosen by the converter’s forming and sealing operation: a deep drawn tray needs O, while a die-cut lid or cap needs H temper.
Because 3003 work-hardens more than pure foil, the temper must match the conversion.
An H-temper web that is then deep-drawn can crack at the corner, while an O-temper web used for a stiff lid may be too soft.
The mill supplies the agreed temper with a certificate, and the converter trials the web before volume.
Degreasing is controlled for food contact in both tempers.
Temper and gauge together define how the web converts. An O web that is too thick drags and wrinkles on the sealing line; an H web that is too thin splinters when die-cut.
Converters usually start from a sample roll of the proposed gauge and temper, run it on their own stamping, sealing or laminating equipment, and adjust before committing to tonnage.
This trial roll is why mills keep sample stock and why the spec must name gauge, temper and end use together rather than as separate choices.
Container and baking foil usually runs 50–150µm, lidding and cap stock around 30–80µm, and thin laminate webs 6–30µm.
Width and core are set by the converter’s slitting and converting equipment, so the mill supplies the jumbo to the agreed gauge, bredde, core and roll weight.
Choosing the gauge is a trade-off between barrier, stiffness and cost.
Heavier foil is stiffer and more puncture-resistant but costs more and is harder to convert; thinner foil is cheaper and softer but weaker and more pinhole-prone.
For formed trays the blank must stretch to the tray depth without necking or splitting, which sets a practical minimum gauge. For lidding, thinner foil seals and peels more easily but must still be pinhole-free to protect shelf life.
The converter’s equipment and the food’s shelf-life requirements, not price alone, should decide gauge.
A jumbo roll is the mill’s wide parent roll; a converter then slits it to narrower rolls, prints or laminates it, or presses it into containers.
Buying jumbo rolls by the tonne is the lowest-cost way for a converter to feed its own slitting, trykning, laminating or container line.
The mill does the rolling, annealing and degreasing; the converter adds value downstream. This is why jumbo rolls are sold to industrial customers, not end consumers.
Quality matters more on a jumbo roll because one defect runs for hundreds or thousands of meters: gauge variation, pinholes, oil stains, edge damage or splices all become converter downtime.
A good jumbo roll is uniform across the width and length, clean, properly wound, and supplied with a lot certificate so the converter can run it without stopping.
Converters also care about hidden spec points: splice count (each splice is a planned stop), winding tension and core hardness so the roll sits true on the unwind, telescope and edge wave so slitting runs straight, and roll stability on the pallet.
These do not show on a material certificate as dramatically as gauge, but they decide whether a high-speed line runs for hours without a break.
A jumbo roll bought only on price can cost more in converter downtime than a better, slightly more expensive roll.
3003 foil starts from cast aluminum alloy ingot with manganese, which is hot-rolled to coil, then cold-rolled repeatedly down to the thin gauge.
Foil gauge is reached by cold rolling and, for light gauges, double-rolling two strands together.
The foil is then annealed—to soften it to O temper or control it to H temper—degased/degreased to remove rolling oil for food contact, and finally slitted and rewound onto cores as jumbo rolls.
Annealing and degreasing are the food-contact-critical steps: annealing sets the temper and softness, while degreasing burns off rolling oil so the surface is clean and food-safe.
Pinhole count, gauge profile, flatness and winding tension are controlled through the line, and each jumbo roll is tested and tied to a lot certificate. Consistent rolling gives the uniform web converters need at high speed.
Pinholes are an inherent foil defect that rises sharply as gauge drops: very thin foil can carry thousands of pinholes per square meter.
The alloy choice matters here—3003’s manganese and the rolling practice reduce pinholes compared with pure foil at the same gauge.
The mill tests pinhole count per lot and reports it, and the converter specifies a maximum acceptable count for barrier-critical jobs.
Too many pinholes and the foil is no longer a complete barrier, so for long-shelf-life laminate and lidding, low pinhole stock is worth paying for.
One of the largest food uses of 3003 foil is formed containers: takeaway trays, airline meal trays, baking pans, roasting tins, loaf pans and disposable food containers.
The web is blanked and deep-drawn or stamped on a container press into the shape. 3003’s strength and rust resistance help the formed tray hold its shape, resist puncture, and survive heat, oil and acidic foods;
O-temper 3003 draws cleanly, while slightly firmer stock gives a stiffer, crisper rim.
Container foil must be clean, degreased and pinhole-free, because a pinhole lets sauce or grease through and a dirty surface fails food-contact rules.
The gauge is usually 50–150µm depending on tray size and whether it is oven-safe. 3003 og 8011 are both used here; 3003 is chosen where a stiffer, more rust-resistant tray is wanted, while soft 8011 is lower cost for light containers.
Container forming works by blanking a disc or rectangle of foil and deep-drawing it over a punch into the die, with a blank holder controlling material flow.
The foil must draw thinly at the corner without splitting, and form a crisp rim.
Springback, earing (the scalloped edge from rolling texture) and orange peel are the defects that show up on formed trays; controlled temper, annealing and a low-earing rolling practice minimize them.
For oven and frozen-food trays, the foil also needs to resist oil, sauce and temperature shock, which 3003’s corrosion resistance supports.
3003 foil is widely used as lidding material: the foil is printed, coated with a heat-seal lacquer, die-cut, and heat-sealed onto yogurt cups, dessert pots, smør, margarine, ready-meal trays, coffee and food cups.
The lidding must peel cleanly, reseal or tear to the consumer’s hand, and keep the food sealed against moisture and oxygen. A stiffer H-temper 3003 web gives a flat, dimensionally stable lid that seals and peels consistently at high speed.
Lidding foil is usually 30–80µm, often laminated or coated with heat-seal lacquer on the food-contact side and printed on the outside.
The web must be flat, clean and free of pinholes so the seal is perfect. Because lidding runs on high-speed form-fill-seal and cup-sealing lines, gauge consistency and edge quality are critical; a sloppy web stops the line.
Lidding is usually a coated or laminated structure rather than bare foil: the foil is coated on the food side with a heat-seal lacquer formulated for the cup material (Pp, Pe, PS), and printed on the outside.
The seal must be strong enough to hold through shipping and cold storage, yet peelable enough for the consumer to open by hand.
The underlying 3003 web provides flatness, stiffness and barrier; the lacquer provides the seal. Bare foil alone does not heat-seal, so converters specify the foil web and then coat or laminate it—which is why a clean, wettable, degreased surface matters.
Tyndere 3003 (og 1235/8011) foil is laminated with plastic films (Pe, Pp, KÆLEDYR) and paper to make the barrier layer in food pouches, poser, coffee bags, snack packaging, retort pouches and foil wraps.
The aluminum layer is the complete barrier to light, ilt, moisture and grease, while the films provide heat-sealing, printability and strength. 3003 is used where the laminate needs extra strength and rust resistance; very thin 6–9µm webs more often use 1235.
For lamination the foil must be degreased and have good surface energy (wettability) so adhesive bonds; a poorly degreased web delaminates.
Pinholes must be controlled, because pinholes in the barrier layer let oxygen through and shorten shelf life.
The jumbo roll is slit to the converter’s laminate width and run through adhesive or extrusion laminating lines.
A typical food laminate is a sandwich such as PET / adhesive / folie / adhesive / Pe: the printed outer PET gives looks and strength, the aluminum foil is the barrier, and the inner PE provides heat-sealing into a pouch.
The foil sits in the middle and is never the heat-seal layer itself. Because the foil is bonded with adhesive, its surface energy (dyne level) after degreasing is as important as its gauge—a low-dyne web delaminates in the field.
Converters therefore specify degreasing and wettability, not just thickness, when buying laminate-grade 3003.
3003 foil webs are also formed into baking sheets, roasting pans, steam-table pans and freezer containers, and supplied as roll or sheet wrap for cooking.
The foil’s heat conductivity and complete barrier make it suitable for oven use, grillning, freezing and storage. 3003’s corrosion resistance helps when the tray contacts marinades, sauces and oily foods, and its stiffness keeps large roasting tins from buckling.
For oven and food-contact use, the degreased, food-safe surface and clean annealing are essential.
Baking trays are often 80–150µm and O-temper for easy forming, while heavy steam-table pans use thicker, stiffer stock.
The foil withstands oven temperatures and freezing without off-flavor transfer.
In commercial kitchens and catering, foil trays are the standard disposable vessel: they go from freezer to oven, hold sauces and oily foods, and are thrown away after use.
This demands a web that resists thermal shock (cold tray into a hot oven), does not leach into acidic tomato or citrus foods, and stays rigid enough to carry without buckling.
3003’s strength and rust resistance fit this duty better than soft pure foil, which is why catering and airline-tray converters often specify 3003 or a 3003/8011 blend for their heaviest disposable trays.
Food grade 3003 foil must be non-toxic, tasteless and odorless, with migration within limits for direct food contact.
This is achieved by controlling the alloy, using food-grade rolling practices, fully degreasing the surface, and providing lot-specific migration or food-contact declarations.
Buyers should request the certificate for the destination market rather than a generic “food grade” claim, and keep the lot number so a container or lid run can be traced back to the coil.
Migration testing measures whether anything transfers from the foil coating or surface into a food simulant.
Bare aluminum foil is one of the most inert food-contact materials, but lacquered, coated or printed foil introduces organic layers, and it is those coatings—not the aluminum—that are tested for migration.
For this reason, a bare O-temper 3003 web has an easier food-contact path than a coated lidding stock; converters doing lidding or printing should confirm that the foil, the lacquer and the ink together meet the destination market’s rules, and keep the coating supplier’s declarations alongside the mill certificate.
On a jumbo roll, the converter checks incoming gauge, pinholes, surface degreasing and edge quality before running it.
A web with too many pinholes fails as a food barrier; an oily web fails lamination and food contact; gauge variation and telescope cause winding problems on the converting line. Lot-specific certificates tie the roll to the alloy, temperament, gauge and food-contact test.
A small incoming inspection at the converter pays off: measure gauge across the width, check a length for pinholes under the light, run a water-break test to confirm degreasing, and inspect the slit edge for burr or curl.
Catching a bad roll at receiving is far cheaper than discovering it mid-run on a sealing or laminating line.
Because each jumbo roll carries a lot number, any dispute can be matched back to the mill’s test records, which is why buying from an integrated mill with real QC—rather than a trader—matters when a batch problem surfaces.
Foil jumbo rolls are moisture-sensitive and scratch-sensitive, so they are wrapped in moisture-proof film with end protectors, packed on wooden pallets or in wooden frames, and clearly tagged with alloy, temperament, gauge, bredde, core, net weight and lot.
Export packing keeps moisture, dirt and edge damage out of the roll during sea freight. Rolls are shipped FOB, CFR or CIF with the mill certificate, food-contact declarations and export documents.
Because thin foil can be dented or edge-damaged, end caps and tight wrapping matter; moisture can cause staining on the coil.
Each pallet is strapped and labeled, and the lot number is kept outside so the converter can trace a roll. Light-gauge food foil is handled with extra care because pinholes and creases are easiest to create on thin material.
On arrival the rolls should be stored dry and indoors, away from moisture, oil and chemicals.
Aluminum itself does not rust in the normal steel sense, but moisture and residual processing chemicals can stain the surface or damage the degreased finish, which matters for food contact and lamination.
Keeping the pallet wrapping until the roll is about to be used, and using first-in-first-out stock rotation, prevents surface degradation. For long sea voyages, desiccants and proper container ventilation reduce condensation inside the package.
Jumbo roll price follows the aluminum ingot base (LME and Shanghai spot) plus rolling, udglødning, degreasing and slitting processing. 3003 is priced slightly above 1xxx because of the manganese and processing, but below specialty pharma foil.
Thinner gauges, tighter tolerances, degreasing for food contact, custom widths and small MOQ raise the unit price; tonnage container orders and standard gauges lower it. Quotes carry a short validity because the metal base moves.
MOQ is typically a tonne or a container for standard gauges and widths; custom widths, cores or temper runs have a smaller minimum and a possible slitting setup.
Buyers control cost by fixing the gauge and width, ordering container quantities, and matching the alloy to the job—using 3003 only where its strength and rust resistance are needed, and softer 8011 or 1xxx for simple wrap.
Buyers often compare quotes on the metal base plus a conversion charge.
The useful comparison is total landed cost: price per tonne, freight, emballage, certificates and—most importantly—expected converter yield.
A slightly cheaper roll with more pinholes, poor degreasing or frequent splices can lower yield and raise labor and scrap cost on the converting line, ending up more expensive than a cleaner premium roll.
For regular food packaging, a qualified mill with consistent lot certificates is usually the lower-cost long-term choice even if its headline price is not the lowest.
State the alloy (3003), temperament (O / H14 / H24), gauge and width, and the end use (container, lidding, laminate, bagning).
Specify the core size, roll weight, surface (bright/matte) and degreasing requirement.
Request food-contact certificates for the target market (FDA, EU 1935/2004, LFGB, GB 4806.9).
Approve a sample roll, confirm gauge, pinholes, degreasing and converting performance.
Confirm price, MOQ, packing and delivery terms, then run production with lot certificates.
Lead time is typically a few weeks for standard gauges and tempers, plus ocean freight to the destination port, with sample rolls sent before bulk commitment.
To keep reorders simple, converters should give the mill a standing spec—alloy 3003, temperament, gauge, bredde, core, surface and a pinhole limit—so every shipment matches the approved sample and line adjustments are not needed each time.
Communication should also cover packaging and documentation: which certificates the consignee needs (FDA, EU 1935/2004, LFGB, GB 4806.9), bill of lading, packing list and commercial invoice, and any food-grade or origin declarations.
A converter that sends its drawing, tray dimensions, cup material or lidding seal requirement up front gets a quotation matched to the job rather than a generic price, and avoids the delay of re-working a web that was not specified tightly enough the first time.
Henan Huawei Aluminium Co., Ltd (HWALU) is a privately owned aluminum manufacturer established in 2001, based in Huiguo Town, Gongyi, Henan—known as China’s Aluminum Capital, in the heart of the country’s aluminum rolling industry.
With around 1,200 employees including a specialist R&D team and a site of about 250,000 kvadratmeter,
HWALU produces more than 200,000 tonnes of aluminum products a year and, as an integrated mill rather than a trader, ruller, anneals, degreases and slits its own foil for customers in more than 70 countries. Office: nr. 52, Dongming vej, Zhengzhou, Henan, Kina.
HWALU manufactures aluminum sheets, coils, folier, strips and circles across the 1000 til 8000 serie, with food and pharmaceutical packaging foil among its core products.
We supply 3003 food grade aluminum foil jumbo rolls alongside 8011, 1235, 8079 og 8021 for food containers, lidding, flexible laminate, baking and bottle-cap stock, in O or H14/H24 temper with a clean degreased surface, controlled pinholes and consistent gauge.
Food-contact certificates, custom width and core, slitting and moisture-proof export packing are available. Email [email protected], or WhatsApp / call +86 18137782032 for a specification-based quotation and production samples.
HWALU supports the whole sourcing loop for food converters: gauge and temper selection for containers, lidding, laminate and baking, draw and sealing samples before volume,
lot-specific mill and food-contact certificates, custom width, core and roll weight, slitting, and consistent reorders held to the same coil spec.
Because we roll, anneal, degrease and slit our own foil rather than reselling other mills, madkvalitet 3003 jumbo rolls arrive clean, low in pinholes and ready for high-speed conversion.
EN: It is Al-Mn alloy foil (about 1.0–1.5% Mn), degreased and certified for direct food contact, stronger and rust-resistant than pure foil.
EN: Bruge 3003 where strength, stiffness and rust resistance matter—formed containers, lidding, caps and baking; use 8011 for soft household wrap and light containers.
EN: O (blød, for deep forming and baking) and H14/H24 (Stiver, til lidding, caps and rigid container edges).
EN: About 6µm up to 200µm; container/baking foil commonly 50–150µm, lidding 30–80µm, thin laminate webs 6–30µm.
EN: Yes—aluminum foil blocks light, ilt, fugtighed, grease and odors, which is why it is the food-barrier layer in laminates and lids.
EN: Lot-specific FDA, EU 1935/2004, LFGB and GB 4806.9 declarations for the destination market.
EN: The wide, large-diameter parent roll sold by the tonne to converters, who slit, print, laminate or press it.
EN: Moisture-proof film with end protectors on wooden pallets/frames, clearly tagged and shipped with full documents.
Food grade 3003 aluminum foil jumbo roll is the right converter material when a food web needs more than soft household foil:
the manganese gives strength, stiffness and rust resistance, so formed containers, cup lidding, bottle-cap stock, baking trays and flexible laminates hold their shape, resist food acids and run reliably at high speed.
O temper suits deep forming and baking; H14/H24 suits stiff lids and caps.
The critical specifications are gauge, temperament, clean degreasing, low pinholes and food-contact certification
all supplied as lot-specific documents by an integrated mill. Sourcing 3003 jumbo rolls from a mill that controls rolling, udglødning, degreasing and slitting gives converters a consistent food barrier that converts cleanly and protects the product through shelf life.
Henan Huawei Aluminium Co., Ltd. er leder af mange aluminiumsproducenter og leverandører i Kina. Vi kontrollerer strengt kvaliteten og fokuserer på kunderne. Vi håber at have et dybtgående samarbejde med dig og give dig højkvalitets aluminiumsmaterialeprodukter tilpassede OEM-tjenester. Hvis du ønsker at få de nyeste og bedste priser pr. kg eller pr. ton standardvægt, kontakt os venligst.